Tag: tolerance

  • GD&T Explained: How Geometric Tolerancing Prevents Manufacturing Disputes

    GD&T Explained: How Geometric Tolerancing Prevents Manufacturing Disputes

    The machinist had machined the part correctly. The inspector had measured it correctly. The design engineer had drawn it correctly. The part still failed incoming inspection at the customer’s facility, which didn’t accept the supplier’s inspection report because their measurements showed a different result. Four weeks of back-and-forth followed: measurement reports, photos, calls across three time zones, and finally a re-inspection visit where everyone sat down together and found the answer.

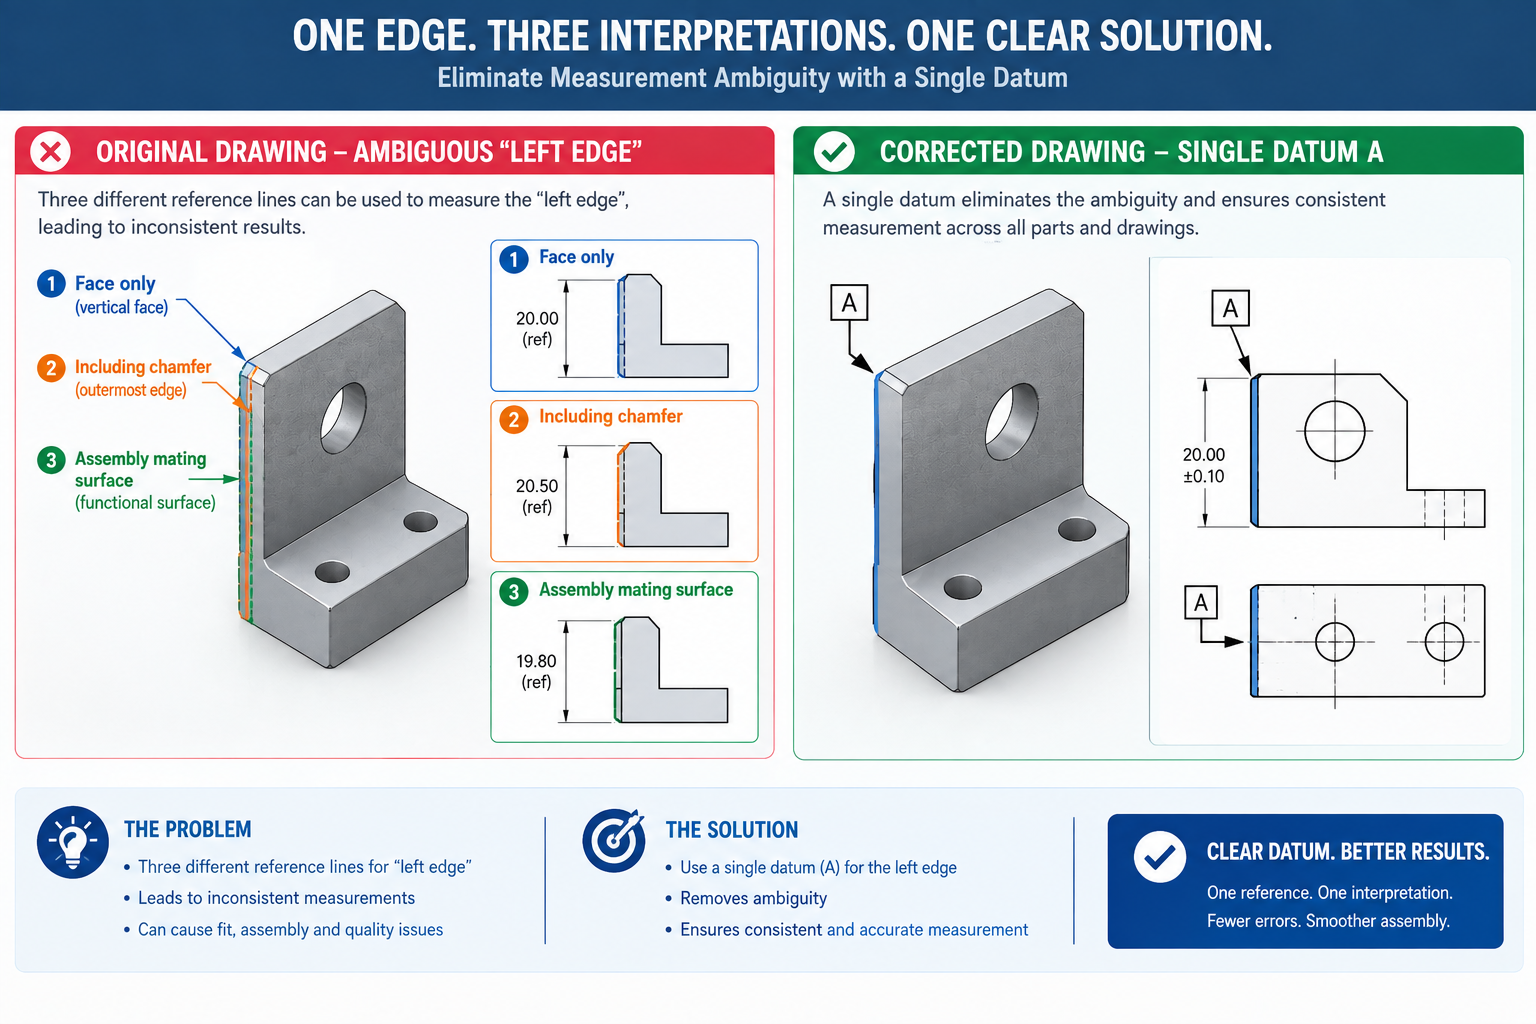
    The drawing specified the hole position from the “left edge” of the part. The machinist had measured from the left face, excluding a small chamfer. The inspector had measured from the left edge including the chamfer. The customer had measured from what they considered the left datum, the mating surface of the assembly. Three different interpretations of two words: “left edge.”

    Quick answer: Geometric Dimensioning and Tolerancing (GD&T) exists to solve exactly this problem. It replaces ambiguous phrases like “left edge” with a datum symbol, a feature control frame, and standardised symbols from ASME Y14.5 or ISO 1101 that mean exactly one thing to everyone trained to read them, in any country, in any language. The dimensions weren’t wrong and the machining wasn’t inaccurate; three experienced professionals just interpreted two words three defensible ways, and GD&T eliminates that gap entirely.
    Diagram comparing three ambiguous interpretations of a left edge dimension versus a single GD&T datum symbol

    This article isn’t a complete GD&T textbook. It’s a practical guide to how GD&T works as a communication tool: the symbol reference covering all fourteen characteristics, the datum selection guide, position tolerance compared against plus-minus coordinates, and worked examples showing what changes on a drawing and what that means for the machinist, inspector, and supplier.

    What GD&T Actually Is and What Problem It Solves

    GD&T is a system of symbols and rules describing the allowable variation in the form, orientation, location, and runout of geometric features on a part. It’s defined by ASME Y14.5 in the United States and ISO 1101 internationally, with the two standards broadly similar in philosophy and substantially compatible in practice. The system replaces or supplements traditional plus-minus coordinate tolerancing, using standardised symbols and feature control frames that carry a complete, unambiguous specification in a compact visual form.

    The problem GD&T solves isn’t just about symbols. It’s about the gap between what a drawing says and what different people understand it to mean. Plus-minus tolerancing specifies a feature’s location by distance from an implied reference. When that reference is clearly defined and everyone measures it the same way, plus-minus works fine. When the reference is ambiguous, or the machinist, inspector, and customer all use slightly different references, the same physical measurement produces different results. GD&T eliminates this by requiring explicit datum definitions, using a three-datum reference frame that specifies the complete geometric relationship between the controlled feature and the references used to measure it.

    The Feature Control Frame: Where All the Information Lives

    The feature control frame is the core element of GD&T on a drawing: a rectangular box read left to right, containing the geometric characteristic symbol, the tolerance value, and one to three datum references. Combined, this contains a complete, self-contained geometric specification that needs no additional note to be unambiguous.

    A feature control frame reading position, 0.15, diameter symbol, datum A, datum B translates to: “the centre of this hole must be within a cylindrical tolerance zone of 0.15mm diameter, oriented perpendicular to datum A and located by true position relative to datums A and B.” Every word of that sentence lives inside the frame, and once you can read the symbols, you can read every feature control frame on every drawing following ASME Y14.5 or ISO 1101.

    The 14 GD&T Characteristics: What Each One Controls

    GD&T defines fourteen geometric characteristics across five categories: form (four, no datum required), orientation (three, datum required), location (three, datum required), runout (two, datum required), and profile (two, datum optional).

    CategoryCharacteristicWhat It ControlsDatum Required?Most Common Application
    FormStraightnessHow straight an axis or surface line element must beNoCylindrical shaft axis; long narrow flat surfaces
    FormFlatnessHow flat a surface must be; deviation from a perfect planeNoSealing surfaces, mating datum faces, PCB mounting pads
    FormCircularityHow round a single cross-section must beNoSealing bores, bearing seats, rotating surfaces
    FormCylindricityHow close to a perfect cylinder the full surface isNoPrecision bearing bores, hydraulic cylinder bores
    OrientationPerpendicularityHow close to 90° a surface/axis is relative to a datumYesBoss faces, shaft axes, mating flange faces
    OrientationAngularityHow close to a specified angle relative to a datumYesAngled faces, tapered holes, dovetail slides
    OrientationParallelismHow parallel a surface/axis is to a datumYesParallel rails, clamp/vice jaw faces, slide guides
    LocationPositionHow far a feature may be from its true theoretical locationYesHole patterns, boss positions; replaces plus-minus for holes
    LocationConcentricityHow close median points are to a datum axisYesOften replaced by runout or position for practical inspection
    LocationSymmetryHow close a median plane is to a datum median planeYesOften replaced by position in modern practice
    RunoutCircular RunoutVariation in a single cross-section as the part rotatesYesRotating shafts, impeller faces
    RunoutTotal RunoutVariation across the entire surface as the part rotatesYesPrecision rotating parts, cam surfaces
    ProfileProfile of a LineVariation of each line element from a true profileOptionalCurved surfaces, aerofoil profiles
    ProfileProfile of a SurfaceVariation of the entire 3D surface from a true profileOptionalComplex freeform surfaces, cast/forged parts, stamped panels

    The Four Most Used Characteristics in Practice

    Four characteristics account for the large majority of GD&T callouts on real drawings:

    Position controls where a feature is located relative to datums, using basic dimensions (boxed, theoretically exact values with no individual tolerance) to define the true position. It’s the most powerful single GD&T tool for hole patterns and boss locations.

    Flatness controls how flat a surface is, independent of any datum, the right tool for sealing faces and mounting bases where overall planarity matters independently of position.

    Perpendicularity controls how close a surface or axis is to 90 degrees relative to a datum, catching tilt that plus-minus height tolerances miss entirely.

    Position with MMC (bonus tolerance) combines position tolerance with the maximum material condition modifier, letting the tolerance zone grow when the feature is produced smaller than its maximum material size. A hole at the upper limit of its diameter tolerance can sit in a less precise position than one at the lower limit, since the larger hole provides more fastener clearance.

    Datums: The Foundation That Everything Else Is Measured From

    Datums are the most important and most frequently misunderstood element of GD&T. Tolerance values attract most of the attention, but they’re only meaningful relative to the datums they reference. A perpendicularity of 0.05mm to datum A is precise if datum A is a well-defined, stable reference surface, and meaningless if datum A is an ambiguous edge different people measure differently. Getting datum selection right matters more than getting the tolerance numbers right.

    Datum TypeWhat It RepresentsCommon MistakeHow to Check It’s Right
    Primary (A)The most stable reference surface; constrains 3 degrees of freedomChoosing a small or convenient CAD surface instead of the actual functional oneWould this part sit stably and repeatably resting on datum A alone?
    Secondary (B)Constrains 2 more degrees of freedom; stops translation and rotationChoosing a secondary parallel to the primary, which gives no independent constraintVisualise the part on A; datum B should stop the direction it can still slide
    Tertiary (C)Constrains the final degree of freedomChoosing a tertiary too close to the secondary for practical measurementShould be as far as practical from the secondary for stability
    Datum feature simulatorThe physical surface (granite plate, mandrel) representing the datum in inspectionAssuming a worn or damaged part surface faithfully represents the datumInspect the datum surface’s own form before using it to measure others
    Axis datumThe axis of a cylindrical feature used as a datumUsing a cylindrical datum with significant form error without specifying its own toleranceVerify roundness and cylindricity of the datum bore/shaft first

    The Functional Datum Principle: Match Datums to How the Part Is Used

    The most important principle in datum selection is choosing datums that reflect how the part is actually located in assembly and used in service, not datums that are convenient to measure or match the CAD coordinate system. A part sitting on a flat base in service should use that base as its primary datum. A part located by a precision bore in assembly should use that bore as its primary datum axis. The inspection setup should mirror the assembly setup as closely as possible.

    When datums are chosen for convenience rather than function, parts can pass inspection and still fail assembly, one of the most frustrating quality failures in manufacturing, because every individual measurement report shows conforming dimensions and the failure only shows up at the assembly line. This is why datum selection belongs to the design engineer, not the inspection department.

    Position Tolerance vs. Plus-Minus: Why the Difference Matters

    Plus-minus coordinate tolerancing is what most engineers learn first, and it’s adequate for a large fraction of dimensions on a typical drawing. But for mating features, particularly hole patterns where multiple features must collectively locate a mating component, it has a well-documented problem: it creates square tolerance zones where circular zones would better match the physical assembly constraint.

    The Square Zone Problem

    A hole position specified as 25.00 +/-0.10 in X and 20.00 +/-0.10 in Y creates a square tolerance zone with 0.2mm sides. A hole accepted at the extreme corner, +0.10 in both X and Y simultaneously, sits at sqrt(0.10² + 0.10²) = 0.141mm from true position, forty-one percent further than either coordinate limit alone suggests. For a round fastener hole, a round zone more accurately represents what actually matters: distance from true position in any direction, not deviation in each coordinate separately.

    GD&T position tolerance specifies the hole location as a diameter of allowable deviation. A position tolerance of 0.2mm diameter means the hole centre must sit within a 0.2mm diameter circle around true position, a maximum deviation of 0.1mm in any direction, exactly matching what a round fastener clearance requires. This circular zone gives 57 percent more usable area than plus-minus of 0.1mm in each coordinate for the same functional clearance.

    SituationPlus-Minus ApproachGD&T Position ApproachWhy GD&T Is Better
    Bolt circle (four holes)X/Y coordinates each +/-0.1mm; square zone per holeSingle position callout, circular zone diameter, referenced to datumSquare zone accepts diagonal positions a round fastener would reject; 57% more usable tolerance area
    Perpendicularity of a bossHeight dimension only; no angularity controlPerpendicularity callout controlling the axis to a cylindrical zone relative to datumPlus-minus height doesn’t catch a boss within height tolerance but tilted 2°, which fails assembly
    Flatness of a sealing faceGeneral tolerance or surface finish note onlyFlatness callout specifying max deviation from a perfect planeA surface can pass individual point tolerances and still be bowed enough to prevent sealing
    Slot position relative to a holeSlot dimensioned from hole centre with plus-minusPosition callout with datum established by the hole; bonus tolerance applies under MMCBonus tolerance gives more slot position tolerance exactly when the locating hole has the most clearance
    Runout of a rotating shaft shoulderDiameter plus-minus; concentricity uncontrolledCircular runout referencing the shaft’s datum axisA shoulder can pass diameter tolerance while significantly eccentric, causing vibration

    Bonus Tolerance and MMC: When the Tolerance Gets Larger

    The maximum material condition (MMC) modifier, a circled M after the tolerance value, formally captures something every experienced assembly engineer knows intuitively: a bigger hole leaves more room for the fastener and doesn’t need to be as precisely located to still work.

    MMC for a hole is its minimum diameter, the condition where the material is at maximum. At MMC, the position tolerance applies exactly as specified. As the hole is produced larger, the position tolerance zone grows by the same amount, this additional allowance is bonus tolerance.

    Worked example: M6 fastener clearance hole
    Specified: 6.5mm diameter, +0.2/-0.0 (range 6.5 to 6.7mm)
    Position tolerance: 0.15mm diameter at MMC
    
    At 6.5mm (MMC): position tolerance = 0.15mm diameter
    At 6.6mm (0.1mm over MMC): 0.15 + 0.10 = 0.25mm diameter
    At 6.7mm (0.2mm over MMC, maximum): 0.15 + 0.20 = 0.35mm diameter
    

    The larger the hole, the more position variation is acceptable, since functional clearance for the fastener increases with hole size. Traditional plus-minus couldn’t capture this without specifying separate position tolerances for different diameter ranges, which nobody does in practice. MMC captures it automatically in a single feature control frame that the machinist, inspector, and customer can all compute and verify identically.

    GD&T as Communication: Five Scenarios Where It Resolves Disputes

    ScenarioWithout GD&TWith GD&TMiscommunication Resolved
    Hole position dispute“25.00 +/-0.10 from left edge”; different edges measured differently; dispute beginsPosition 0.20mm diameter zone from datum A, B; everyone measures the same referenceThe datum removes the “which edge” question entirely
    Supplier interpreting perpendicularity“Perpendicular within 0.05mm”; supplier asks over what length, to which surface; days of delayPerpendicularity 0.05mm cylindrical zone to datum A; complete answer in the symbolThe feature control frame answers length, reference, and geometry without a phone call
    Inspector accepting/rejecting a partEach coordinate individually within limits but combined deviation is unclear; judgement callPosition tolerance gives a single diameter comparison against measured deviation; clear pass/failGD&T removes the grey zone where parts pass each coordinate but fail combined deviation
    Planning a machining sequenceDimensions from different references; machinist guesses which surface to cut firstClear datum hierarchy A-B-C tells the machinist the foundation surface to cut firstThe datum hierarchy expresses the designer’s intended machining sequence directly
    Cross-border supplier, first drawingCompany-specific shorthand and language-specific notes generate eight clarification callsStandard ASME Y14.5 symbols readable by any trained engineer, any countryGD&T’s symbol language needs no translation or clarification

    The Cross-Border Supplier Scenario

    International supply chains are where GD&T’s role as a universal language matters most. A drawing with text notes in English, company-specific abbreviations, and implied references understood within one engineering team isn’t self-contained once it travels to a supplier who speaks a different first language and works within a different drawing tradition. A drawing using GD&T consistently, with every geometric requirement in feature control frames referencing defined datums, is readable by anyone trained in ASME Y14.5 or ISO 1101 regardless of native language. A well-written GD&T drawing is its own translator.
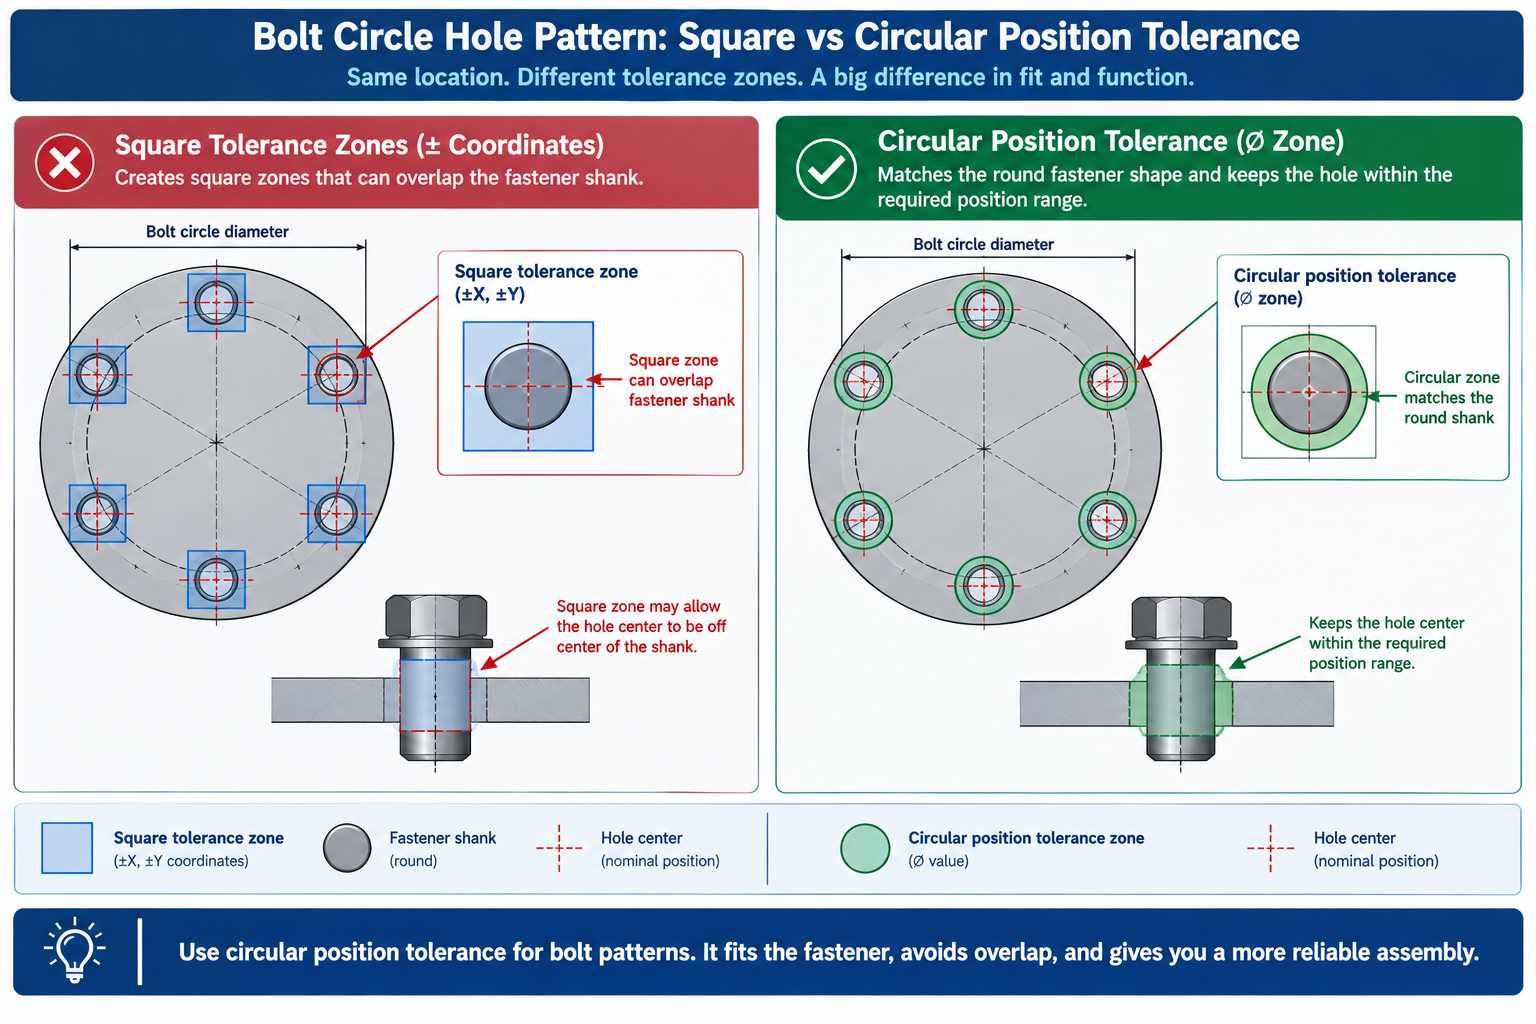
    Comparison of square plus-minus tolerance zones versus circular GD&T position tolerance zones for a bolt circle hole pattern

    Common GD&T Mistakes That Undermine Communication

    Specifying a GD&T tolerance without the required datum. Position, perpendicularity, angularity, and all orientation and location characteristics require a datum reference to be meaningful. A position callout without a datum defines the tolerance zone’s size but not its location in space, forcing the machinist to guess, recreating the exact ambiguity GD&T exists to prevent. Every location or orientation feature control frame needs at least one datum reference.

    Applying GD&T to features that don’t need it. Every feature control frame adds reading complexity, requiring the reader to identify the characteristic, tolerance, and datums and understand how they combine. For features where a simple plus-minus dimension is adequate and unambiguous, like the overall length of a non-mating handle, adding a profile callout adds complexity without adding information. Reserve GD&T for features where its specific capabilities, circular zones, datum-referenced orientation, flatness independent of position, add something plus-minus can’t provide.

    Choosing datums that don’t match the assembly setup. A datum scheme using the most convenient measurement surfaces rather than the surfaces that actually locate the part in assembly produces parts that pass inspection and fail assembly. This failure is invisible at the symbol level, the drawing can be technically correct in its GD&T application and functionally wrong in its datum structure, since the technical correctness shows in the drawing and the functional incorrectness only shows up when assembly fails.

    Worked Examples

    The bolt circle that failed assembly: A machined aluminium flange had eight M8 clearance holes on a 120mm pitch circle, specified by X-Y coordinates with plus-minus 0.15mm each direction. The mating flange used the same approach. Parts passed incoming inspection individually, but assembly consistently produced one misaligned hole pair requiring bolts to be forced or holes filed open.

    The square tolerance zones allowed holes up to 0.212mm from their true circular positions. Two holes on opposite flanges, each at the maximally misaligned corner but in different directions, combined for up to 0.424mm misalignment, which the M8 clearance hole’s 0.5mm total clearance couldn’t reliably absorb.

    Redesigning with a true position tolerance of 0.20mm diameter at MMC, referenced to the flange face and central bore, replaced the coordinate approach with a polar position control tied to the flange’s actual locating features. Maximum deviation of any hole from true position dropped to 0.10mm, and MMC allowed additional tolerance when holes were larger than minimum size. Combined maximum misalignment between matching holes dropped to 0.20mm, comfortably within the 0.5mm clearance. Assembly interference issues were eliminated, and the drawing got simpler: one basic radius, one basic angular spacing, and one feature control frame replaced sixteen coordinate dimensions.

    The supplier dispute that never happened: A design team releasing a machined bracket to an overseas supplier for the first time had previously spent three weeks resolving a dispute with a different supplier over a “top face” reference for mounting hole positions, resulting in batch rejection and rework.

    For the new release, the largest mounting face became datum A with a flatness callout of 0.03mm, the perpendicular face became datum B with a perpendicularity callout of 0.05mm to A, and the mounting holes carried position tolerance of 0.15mm diameter at MMC referenced to A and B, with basic dimensions defining their theoretically exact positions. The new supplier machined a first article within the stated lead time, referencing the same datums as the drawing, with no questions about “top face” since datum A was explicit. The first article was accepted on first inspection with zero dispute calls.

    Frequently Asked Questions

    Do I need to use GD&T on all dimensions, or just some? GD&T is most valuable on dimensions controlling mating features: hole positions for bolt circles and locating pins, surface flatness for sealing and mounting faces, perpendicularity for assembled flanges, and runout for rotating surfaces. Non-mating dimensions with no geometric locating function are adequately controlled by plus-minus with a clear general tolerance note. Over-applying GD&T to every dimension adds drawing complexity without adding communication quality.

    What is the most important GD&T characteristic to understand first? Position tolerance, since understanding it requires understanding three things underpinning all of GD&T: basic dimensions, datum reference frames, and the difference between a circular and square tolerance zone. Once position is clear, perpendicularity, angularity, and parallelism are straightforward extensions of the same logic. Flatness is easiest to understand on its own since it needs no datum, but it’s less central to the broader framework than position.

    What is bonus tolerance and when does it apply? Bonus tolerance is additional position tolerance available when a feature is produced at a size other than its maximum material condition. For a hole, MMC is the minimum diameter; producing it larger grows the position tolerance zone by the same amount, reflecting that a larger hole can sit in a less precise location and still assemble correctly. Bonus tolerance only applies when the MMC modifier appears in the feature control frame; without it, position tolerance stays fixed regardless of actual feature size.

    Why does GD&T use basic dimensions instead of normal toleranced dimensions? Basic dimensions are theoretically exact nominal values carrying no individual tolerance, because the feature’s allowable variation is carried entirely by the feature control frame. If basic dimensions had their own tolerances, the actual allowable variation would combine two separate tolerances with ambiguity about which governs. Basic dimensions remove that: the true position is exactly what the dimension says, and the feature control frame states how far the actual feature may deviate.

    How do I choose between profile of a surface and other characteristics for a complex shape? Profile of a surface is the most versatile characteristic, controlling form, orientation, and location simultaneously. For simple flat, cylindrical, or spherical surfaces, a specific form, orientation, or location characteristic is usually clearer and easier to inspect. For complex freeform surfaces, cast housings, aerofoil sections, stamped panels, profile of a surface is often the only practical way to specify the requirement, since no simpler characteristic captures the 3D variation.

    Can GD&T be applied to 3D models instead of 2D drawings? Yes, increasingly common through Model-Based Definition (MBD). GD&T annotations attach directly to 3D CAD model features using the same feature control frame symbology and datum structure as a 2D drawing, creating a single authoritative source for geometry and tolerances. ASME Y14.41 defines the standard for digital product definition, and most major CAD packages support MBD annotation. The underlying concepts, datums, feature control frames, basic dimensions, bonus tolerance, are identical whether applied on a drawing or in a model.
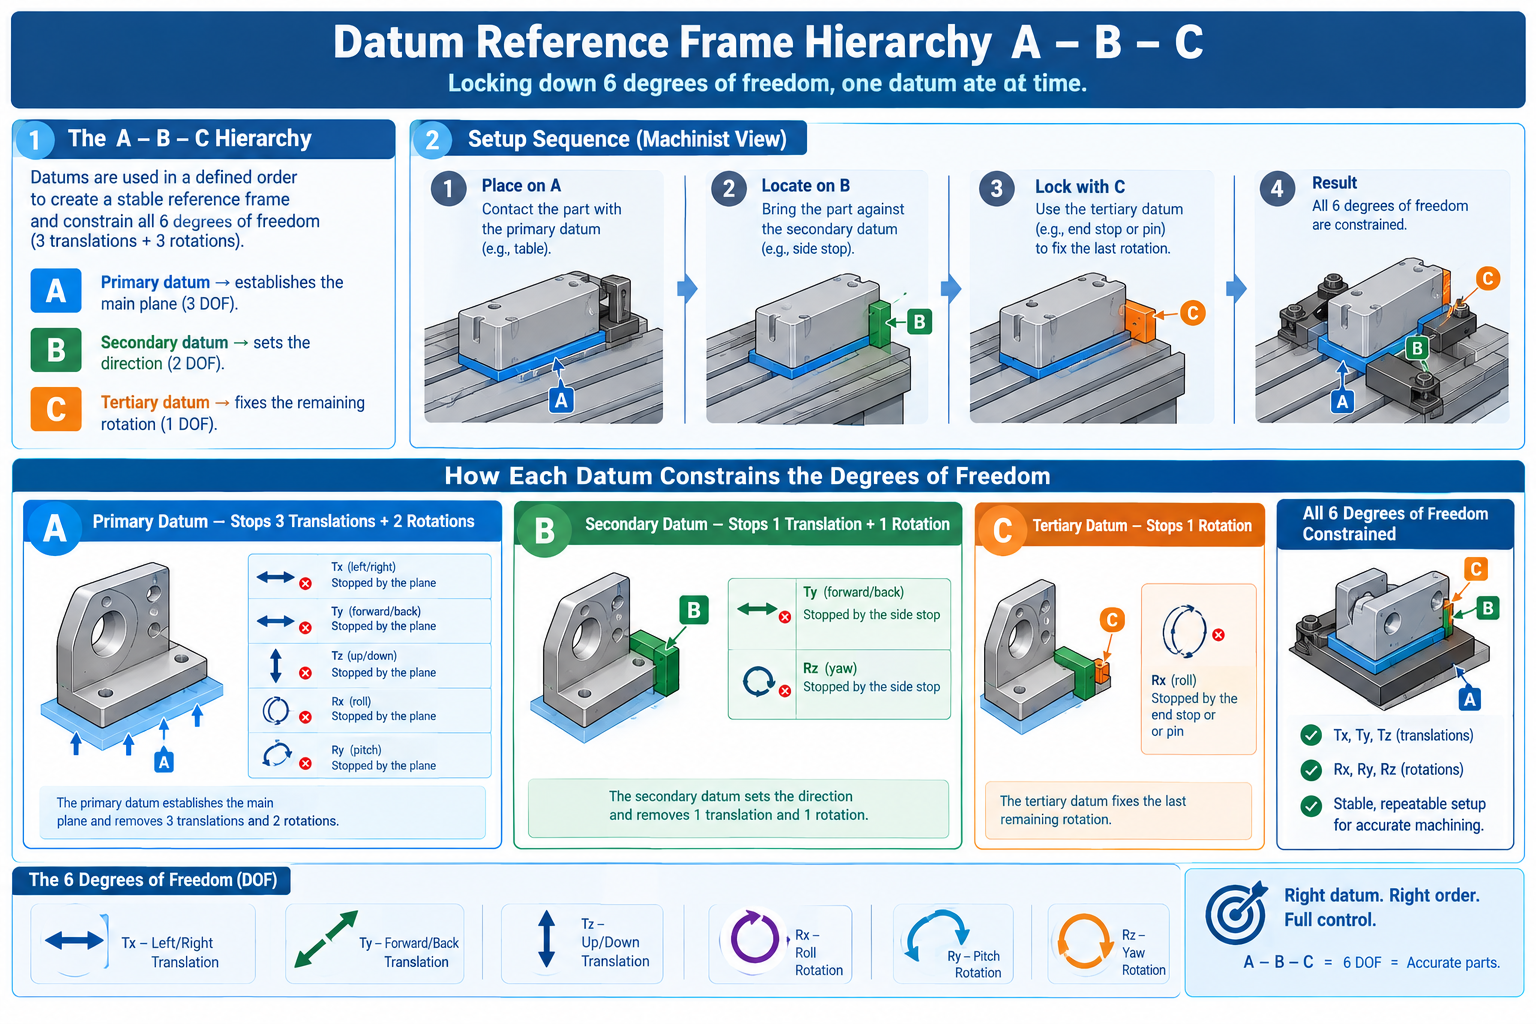
    Diagram showing the primary, secondary, and tertiary datum reference frame constraining six degrees of freedom for machining setup

    Key Takeaways

    The four-week dispute from the opening story ended with everyone agreeing the drawing should have been clearer about which edge was the datum. That agreement, reached after four weeks and a re-inspection visit, is exactly what a GD&T datum symbol would have enforced from the start, at no additional cost beyond the seconds it takes to place a datum symbol on a drawing.

    GD&T isn’t complicated once the core concepts are clear. Feature control frames have a fixed structure. The fourteen characteristics each control one specific geometric property. Datums are chosen to match the assembly function. The communication quality from a consistently applied GD&T drawing is proportional to the functional clarity of the datum structure and the appropriateness of the characteristics chosen, not to the number of callouts or the tightness of the tolerance values.

    The engineers who benefit most from GD&T aren’t the ones who memorise the most symbols. They’re the ones who understand the principle well enough to choose datums that match the assembly function, apply position tolerance where a circular zone better represents the requirement than a square one, and use flatness instead of a surface finish note when planarity, not roughness, is what governs performance. That understanding converts GD&T from drawing notation into a genuine communication tool between design, manufacturing, and inspection, one that prevents disputes rather than generating them.
  • Engineering Drawing Standards: ASME, ISO, and DIN — What Is the Difference?

    Engineering Drawing Standards: ASME, ISO, and DIN — What Is the Difference?

    86%  of US engineering companies use ASME Y14.5 as their GD&T standard (Krulikowski survey, 133 respondents across 27 countries)
    56%  of non-US international companies also use ASME Y14.5, making it the most-used GD&T standard globally despite ISO GPS being the international standard
    100+  individual modular standards in the ISO GPS family, compared to approximately 17 documents in the ASME Y14 series
    R2024  ASME Y14.5-2018 reaffirmed in 2024, confirming it remains the current ASME GD&T standard. No new revision is in force as of 2026.

    Introduction:

    A machined shaft is designed in the United States under ASME Y14.5. The purchase order goes to a precision machinist in Germany who works exclusively to DIN EN ISO standards. The drawing arrives. The machinist reads the cylindricity tolerance as independently controlled, as ISO 8015 requires, and machines the shaft to those standards. The shaft arrives in the US. Inspection rejects it because under ASME’s envelope principle, the size tolerance was supposed to control the cylindricity automatically, and the part’s form errors fall outside what the ASME-reading inspector considers acceptable.

    Nobody did anything wrong. The drawing was correct. The machinist was correct. The inspector was correct. The problem was that the drawing did not state which engineering drawing standard governed its GD&T, and the two parties operated under different default assumptions about what the same symbols and tolerance values meant.

    This guide explains what ASME, ISO, and DIN drawing standards are, how they differ technically and philosophically, which industries and geographies use which, and what the specific conflicts are between standards that cause parts to be made or inspected incorrectly when engineers do not know which standard applies.

    Quick answer:  ASME Y14.5 is the US standard for GD&T and engineering drawings, using third-angle projection and the envelope principle by default. ISO GPS (ISO 1101 and related standards) is the international standard, using first-angle projection and the independency principle. DIN standards are German national standards that have largely been harmonised with ISO since the 1990s and are now cited as DIN EN ISO in most cases. All three must be explicitly stated in the drawing title block because mixing them without notation causes misinterpretation of tolerances and views.
    Engineering Drawing Standards ASME, ISO, and DIN
    Always check the projection symbol in the title block before reading any view on a drawing from an unfamiliar source.

    ASME, ISO, and DIN: What Each Standard System Actually Is

    ASME: The American Engineering Drawing Language

    ASME stands for the American Society of Mechanical Engineers, a non-profit professional organisation founded in 1880. Its Y14 series of standards defines how engineering drawings are produced and interpreted in the United States. The most important of these is ASME Y14.5, which defines GD&T: the symbolic language for communicating dimensional requirements and tolerances.

    ASME Y14.5 can trace its roots to MIL-STD-8, a US military standard from 1949. It was the wartime need for interchangeable parts produced at multiple facilities that drove the early development of formalised geometric tolerancing. The standard has been revised approximately every decade since the 1960s. The current version is ASME Y14.5-2018, reaffirmed in 2024 (designated R2024), confirming it remains in force. No newer revision is in effect as of 2026.

    The 2018 edition made two changes that every engineer working to ASME standards should know: it deprecated the concentricity and symmetry symbols, replacing them with positional or profile controls, and it explicitly incorporated Model-Based Definition (MBD), recognising that tolerances are increasingly embedded in 3D models rather than printed on 2D drawings.

    ISO GPS: The International Drawing Language

    ISO is the International Organization for Standardization, founded in 1947. Its ISO GPS system (Geometrical Product Specifications) is the international framework for engineering drawing standards, covering everything from line types (ISO 128) to surface texture (ISO 1302) to the full GD&T system (ISO 1101, ISO 8015, and over 100 related standards).

    Unlike ASME’s relatively consolidated Y14 series of around 17 documents, the ISO GPS system is modular and composed of more than 100 interrelated standards, each covering a narrow, specific aspect of geometric specification. ISO 1101 covers tolerancing symbols. ISO 8015 defines the fundamental rules. ISO 5459 covers datum references. ISO 14638 defines the masterplan for the GPS system. This modularity is both a strength, each standard can be updated independently, and a challenge, because understanding the full system requires familiarity with multiple documents.

    ISO GPS is the default standard in Europe, increasingly adopted in Asia, and the required standard for international supply chains that cross multiple regulatory jurisdictions. Its first-angle projection convention and independency principle for tolerancing represent fundamentally different default assumptions from ASME.

    DIN: The German National Standard

    DIN stands for Deutsches Institut fur Normung, the German Institute for Standardization, founded in 1917. DIN standards for engineering drawings have been through significant harmonisation with ISO since the 1990s as part of European standardisation efforts. The consequence is that most current DIN engineering drawing standards are designated DIN EN ISO, meaning they are the German national adoption of a European (EN) adoption of an International (ISO) standard.

    The practical meaning: DIN EN ISO 1101 is the same standard as ISO 1101 in technical content. DIN EN ISO 2768 is the same as ISO 2768. When a German supplier cites DIN EN ISO standards, they are working to the same technical requirements as any other ISO GPS user. The DIN-specific designation indicates the standard has been formally adopted as a German national standard, which carries regulatory significance in some procurement contexts.

    Where DIN remains genuinely distinct is in standards that have not been harmonised, such as DIN 7168 (German general tolerances, which differs from ISO 2768 in some tolerance classes), older DIN standards that remain in use in specific industries, and VDA (Verband der Automobilindustrie) supplementary standards for German automotive supply chains that have no direct ISO equivalent.

    AttributeASME (Y14 series)ISO (GPS system)DIN (German standard)
    Governing bodyAmerican Society of Mechanical EngineersInternational Organization for StandardizationDeutsches Institut fur Normung (German Institute for Standardization)
    Primary geographyUSA, Canada, parts of AsiaEurope, Asia, global baselineGermany, Austria, German-speaking markets
    GD&T standardASME Y14.5-2018 (R2024)ISO 1101, ISO 8015, 100+ GPS standardsDIN ISO 1101 (mirrors ISO GPS)
    Projection methodThird-angle projection (ANSI)First-angle projection (ISO)First-angle projection (ISO-aligned)
    Line standardsASME Y14.2ISO 128DIN ISO 128
    Title block standardASME Y14.1ISO 7200DIN 6771
    Tolerance philosophyEnvelope principle (Taylor principle)Independency principle (ISO 8015)Independency principle (ISO-aligned)
    Default for dimensionsAll dims controlled by size limitsForm error independent of sizeForm error independent of size
    Standards structure~17 documents in Y14 series100+ modular GPS standardsAligned to ISO, with German national supplements
    Industry dominanceAerospace, defence, US automotiveEuropean mfg, pharma, global supplyGerman automotive (VDA), machinery, industrial

    Third-Angle vs First-Angle Projection: The Most Visible Difference

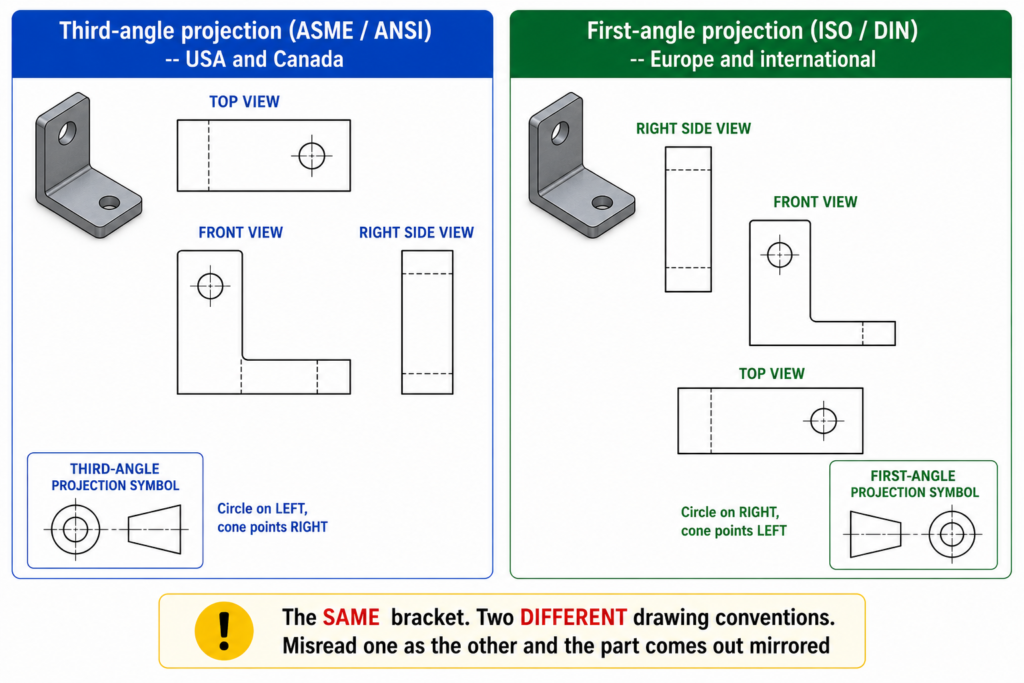
    This is the difference that causes the most obvious manufacturing errors when it is not checked. The projection method determines where each view sits on the drawing sheet relative to the front view, and getting it wrong means reading a right side view where a left side view should be, and vice versa.

    AspectThird-angle projection (ASME / ANSI)First-angle projection (ISO / DIN)
    Where views sitView placed on the side you look from. Right side view sits to the right of front view.View placed on the opposite side. Right side view sits to the LEFT of front view.
    Top view positionTop view sits ABOVE the front viewTop view sits BELOW the front view
    Identification symbolCircle on left, cone pointing rightCircle on right, cone pointing left
    Dominant standardUSA, Canada, Australia (some use)Europe, Asia, rest of world
    Risk of confusionReading first-angle as third-angle produces mirrored or inverted partsSame risk applies in reverse for non-European readers
    Where statedAlways in the title blockAlways in the title block
    Critical checkConfirm before reading any drawing from an unfamiliar sourceNever assume. Always check the projection symbol in the title block first.

    The projection symbol in the title block is small and easy to overlook. It is also the single most important piece of information on the drawing for anyone who has not worked with both systems. An engineer trained exclusively in ASME drawings, reading a European supplier’s first-angle drawing without checking the symbol, will consistently misidentify which side of the part each view shows.

    The manufacturing consequence of projection confusion:  A bracket designed with a mounting boss on the right side, read from a first-angle drawing by an engineer expecting third-angle, will be interpreted as having the boss on the left side. The machinist machines what the drawing appears to show. The part is wrong. By the time it is discovered, the setup, material, and machining time are wasted. The root cause is not the drawing. It is failing to check the projection symbol before reading the views.

    Envelope vs Independency: The Most Important Technical Difference

    This is the difference that causes the most subtle and expensive manufacturing problems when standards are mixed, because the same tolerance value means something different depending on which principle applies. A 25mm shaft toleranced at plus or minus 0.1mm under ASME and the same shaft under ISO are not the same specification, even though the numbers are identical.

    AspectEnvelope Principle (ASME Y14.5)Independency Principle (ISO 8015 / DIN)
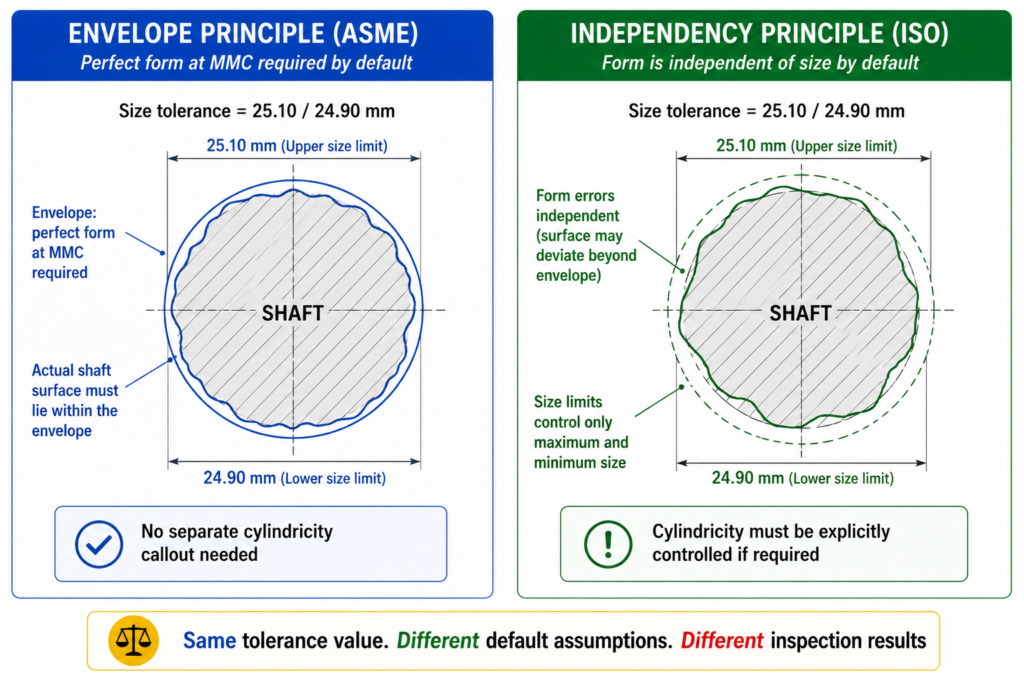
    What it meansThe size tolerance automatically controls form. A 25mm +/-0.1mm cylinder may not exceed a perfect 25.1mm envelope at any cross-section.Size and form are independent. A 25mm +/-0.1mm cylinder may be anywhere between 24.9mm and 25.1mm at any cross-section, but form errors must be separately controlled.
    Who controls form errorsThe size limits do this automatically for ASME drawings without extra symbolsForm errors (straightness, cylindricity, flatness) must be explicitly called out with GD&T symbols
    Effect on designFewer symbols needed for simple prismatic featuresMore symbols required to fully constrain form, but intent is more explicit
    Effect on inspectionEnvelope gauge checks form and size simultaneouslyForm and size inspected separately unless combined control is explicitly stated
    Which standard appliesASME Y14.5 (default, unless E modifier reverses it)ISO 8015 (default for ISO drawings). ASME can invoke ISO 8015 using the E modifier.
    Risk of misinterpretationAn ISO-trained inspector may not apply the envelope check on an ASME drawingAn ASME-trained inspector may assume form is controlled when it is not on an ISO drawing

    A Practical Example of the Difference

    An ASME drawing specifies a shaft diameter of 25.00mm plus or minus 0.10mm. Under the envelope principle, this means the shaft must pass through a perfect 25.10mm ring gauge (the maximum material boundary) and must be no smaller than 24.90mm anywhere. The ring gauge check automatically verifies that the shaft is straight and circular within the size tolerance. No separate cylindricity callout is needed.

    The same shaft on an ISO GPS drawing with the same diameter tolerance of 25.00mm plus or minus 0.10mm operates under the independency principle. The shaft may be anywhere between 24.90mm and 25.10mm at any cross-section, but the form errors (how straight and circular it is) are not controlled by the size tolerance. If the shaft must also be straight within a certain tolerance, a separate straightness callout is required. If cylindricity must be controlled, a cylindricity callout is required.

    GD&T principles comparison Envelope Principle vs Independency Principle
    The envelope vs independency difference is invisible on the drawing unless you know which standard applies.
    The practical result: a shaft manufactured to the ASME specification may have better form control than required by ISO, or an ISO shaft may have worse form than an ASME-trained inspector expects. Both are correct for their respective standards. Neither is wrong. But if an inspector trained in ASME applies the envelope principle to an ISO-drawn part, they may accept or reject parts incorrectly.

    GD&T Symbol Differences Between ASME and ISO: Where Conflicts Actually Live

    Most are identical between ASME Y14.5 and ISO 1101. The flatness symbol, the straightness symbol, the angularity symbol, the position symbol: all use the same geometric shapes with the same meaning. This convergence has been deliberate and sustained over decades of parallel standard development. The conflicts that exist are important precisely because they are not obvious from a visual scan of the symbols.

    Feature / SymbolASME Y14.5ISO GPS (ISO 1101)Practical consequence of mixing
    FlatnessFlatness symbol (parallelogram)Same symbol, different default scopeBoth use same symbol but ISO requires explicit callout where ASME uses envelope rule
    CylindricityExplicit callout requiredExplicit callout requiredNo difference in symbol, significant difference in when it is needed
    Position (Location)True position symbol, bidirectionalSame symbol, ISO may use differentlyAlways verify datum scheme matches between supplier and buyer
    Datum feature symbolFilled triangle on leaderSame but triangle placement differsDatum A may point to different surface if convention not stated
    AngularityAngularity symbolSame symbolNo symbol conflict, same interpretation
    ConcentricityIn ASME Y14.5-2018: deprecatedStill used in ISOCritical conflict: ASME has removed this symbol. ISO still uses it.
    SymmetryIn ASME Y14.5-2018: deprecatedStill used in ISOCritical conflict: same as concentricity situation above.
    RunoutCircular and total runoutCircular and total runoutSame meaning, same symbols, no conflict
    Projected tolerance zonePTZ modifier in ASMEISO uses P modifier differentlyPTZ application differs between standards. State standard on drawing.
    Surface texture (Ra)ASME B46.1ISO 1302 / ISO 4287Both use Ra value but measurement method and filtering can differ

    The Concentricity and Symmetry Deprecation: A Live Conflict

    The most significant current conflict between ASME and ISO GD&T symbol sets is the deprecation of concentricity and symmetry in ASME Y14.5-2018. These symbols remain in active use in ISO GPS drawings and are taught in ISO-based GD&T training globally.

    In ASME Y14.5-2018, both were removed and replaced by position or profile of a surface controls, which Subcommittee 5 argued were more precisely defined and more readily inspectable. The argument has merit: concentricity as defined required deriving a median point from every diametrically opposed pair of points on the surface, which is mathematically rigorous but metrologically challenging.

    The practical consequence for engineers: if you receive a drawing with a concentricity symbol and you are working to ASME Y14.5-2018, the symbol is formally undefined in your standard. If the drawing states ISO 1101 as its reference, the symbol is valid and means what it says. If the drawing states nothing, you have no way of knowing which interpretation to apply without asking. This is exactly the situation the title block note requirement is intended to prevent.

    Key Engineering Drawing Standards: Complete Reference Table

    The table below provides a quick reference to the most important engineering drawing standards across all three systems, covering what each standard covers and its current status.

    StandardBodyYear / StatusWhat it covers
    ASME Y14.5ASME2018 (R2024)Geometric dimensioning and tolerancing: all GD&T symbols, datum references, tolerance zones
    ASME Y14.1ASMECurrentDrawing sheet sizes, title block format, and drawing format requirements
    ASME Y14.2ASMECurrentLine conventions and lettering for engineering drawings
    ASME Y14.41ASMECurrentDigital product definition data practices (MBD, 3D annotation)
    ASME Y14.100ASMECurrentEngineering drawing practices: completeness, approval, revision control
    ISO 128ISOISO 128-1:2020General principles for technical drawings: line types, projections, views
    ISO 1101ISOISO 1101:2017Geometrical tolerancing: symbols, definitions, tolerance zones (ISO GPS core standard)
    ISO 8015ISOISO 8015:2011Fundamentals of tolerancing: independency principle, ISO default rules
    ISO 2768ISOISO 2768-1/2General tolerances for linear and angular dimensions (medium m, fine f classes)
    ISO 7200ISOISO 7200:2004Title block format and data fields for technical drawings
    ISO 1302ISOISO 1302:2002Surface texture indication on technical drawings (Ra, Rz symbols)
    ISO 10628ISOISO 10628-2:2012Symbols for process plant diagrams (P&IDs and flow diagrams)
    DIN 6771DINCurrentGerman title block standard, supplementary to ISO 7200
    DIN ISO 1101DINMirrors ISO 1101German national adoption of ISO geometrical tolerancing standard
    DIN 7168DINCurrentGerman general tolerances for linear and angular dimensions (precedes ISO 2768)
    DIN EN ISO 2768DINCurrentGerman adoption of ISO 2768 general tolerances, often still cited as DIN 2768
    Practical rule for cross-border drawings:  When creating a drawing that will be manufactured outside your home country, look up whether the standards you are referencing are recognised by your supplier’s standards system. Most ASME standards are not formally adopted in Europe. Most ISO standards are available in the USA but not universally taught or enforced. When in doubt, state all relevant standards explicitly in the general notes and confirm with the supplier’s quality team that they hold the referenced documents.

    General Tolerances: ISO 2768, DIN 7168, and the ASME Approach

    General tolerances are the tolerances that apply to all undimensioned or untoleranced features on a drawing, defined by a single title block reference rather than individual callouts. They are one of the most frequently misunderstood elements of cross-standard drawing practice.

    ISO 2768: The International General Tolerance Standard

    ISO 2768 defines general tolerances for linear and angular dimensions in two parts. ISO 2768-1 covers linear dimensions and angles in four classes: fine (f), medium (m), coarse (c), and very coarse (v). ISO 2768-2 covers geometrical tolerances in three classes: H, K, and L. A drawing referencing ISO 2768-mK in its general notes is specifying medium-class linear tolerances and K-class geometrical tolerances for all features not individually dimensioned.

    ISO 2768 medium (m) is the most commonly specified class for general machined parts and represents what most competent machine shops can hold in production without special process controls. Fine (f) requires tighter process discipline and is appropriate for precision assemblies. The class should be chosen to match the actual manufacturing process capability of the supplier, not to the tightest possible requirement.

    DIN 7168 and DIN 2768: The German Predecessors

    DIN 7168 is the German general tolerance standard that predates ISO 2768 and covers similar ground with some different tolerance class definitions. Many older German engineering drawings reference DIN 7168 rather than ISO 2768. The two are not identical in all tolerance class values, which means a drawing referencing DIN 7168 fine and a drawing referencing ISO 2768-f are not necessarily specifying the same tolerances on every feature.

    DIN 2768 is frequently cited in engineering contexts but refers to the German national adoption of ISO 2768, technically designated DIN EN ISO 2768 in its current form. For practical purposes, DIN EN ISO 2768 and ISO 2768 are technically equivalent. DIN 7168 is the historically distinct German standard that should not be assumed equivalent to ISO 2768 without checking the specific tolerance values.

    ASME and General Tolerances

    ASME does not use ISO 2768. The ASME approach to general tolerances is different: ASME Y14.5 provides for general tolerance notes in the title block that define plus/minus values for specific dimension ranges, and ASME Y14.100 covers drawing practices including default tolerances. An ASME drawing with a title block note reading ‘3-place decimals: plus/minus 0.005 inch’ is applying a general tolerance, but under a completely different framework from ISO 2768.

    An engineer moving from an ISO GPS environment to an ASME environment cannot assume that referencing ISO 2768 is meaningful on an ASME drawing. It is not part of the ASME drawing practice system. The general tolerances must be expressed using ASME-compatible notation.

    Which Industries Use Which Standards: The Real-World Map

    Standard selection in most organisations is driven by customer requirements, regulatory obligations, and the geographic location of the primary manufacturing base, not by any abstract technical preference. Understanding which standards dominate which industries tells you immediately which standard to use for a given project.

    IndustryDominant standardReasonTypical supplementary standards
    US Aerospace and DefenceASME Y14.5-2018MIL-STD heritage, US OEM requirementAS9100, ASME Y14.100, ASME Y14.41 for MBD
    European AerospaceISO GPS (EN 9100 aligned)EU OEM and EASA regulatory chainISO 10135, ISO 1302, NADCAP quality reqs
    German Automotive (VDA)DIN / ISO GPS + VDA normsVDA 2 quality and DIN tool standardsVDA 2, VDA 6.1, DIN 7168, DIN ISO 2768
    US Automotive (AIAG)ASME Y14.5 + AIAGBig-Three OEM supply chain standardAIAG PPAP, MSA, FMEA documentation
    Medical devices (FDA)ASME or ISO by choiceFDA 21 CFR Part 820 references bothISO 13485, FDA guidance on drawings
    Pharmaceutical (EU GMP)ISO GPS preferredEU GMP and EMA regulatory alignmentEU GMP Annex 15, ISO 9001
    Industrial machineryISO / DIN (Europe)EN machinery directive complianceISO 4156, DIN 7168 general tolerances
    Consumer electronicsISO or ASME by regionDepends on where manufactured / soldIPC standards for PCB, ISO 2768 general
    Oil and gas (ASME PCC)ASME B31, API standardsASME pressure vessel and piping codesAPI 6A, ASME B16.5, ASME VIII Div 1

    The US Dominance of ASME in a Global Market

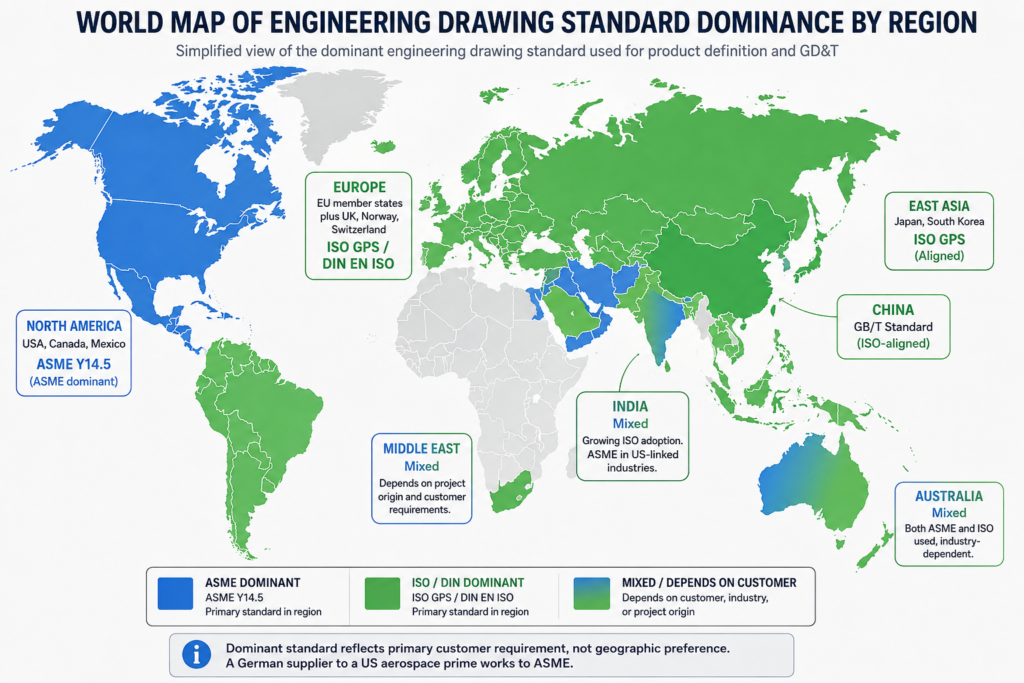
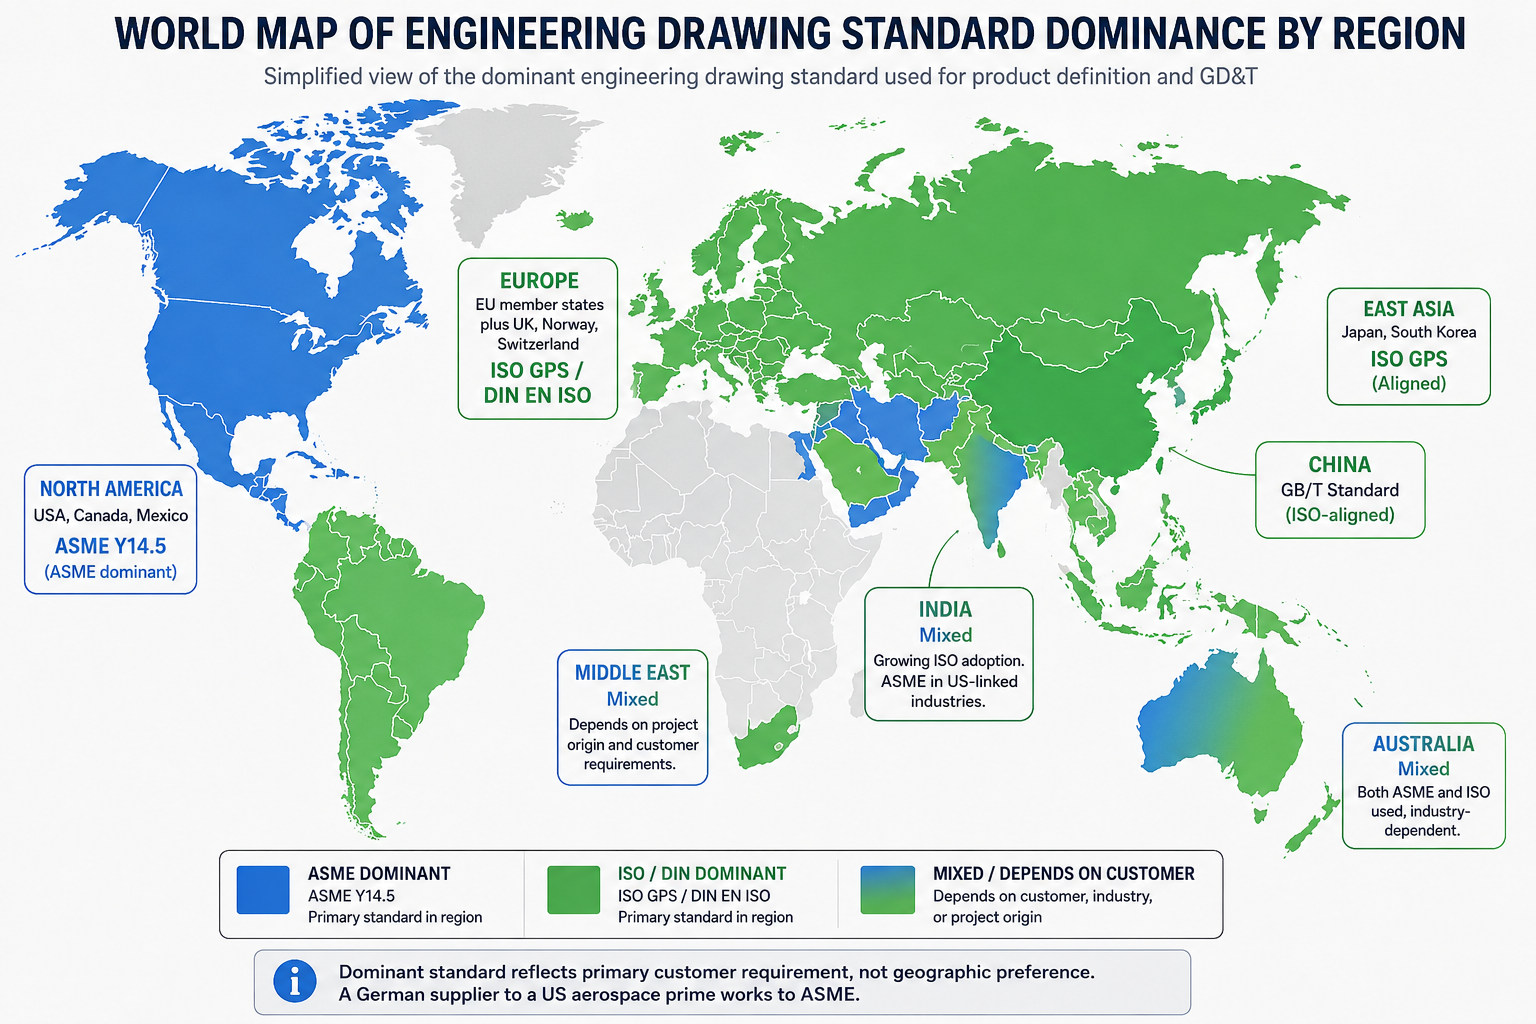
    The survey data from GD&T educator Alex Krulikowski, with 133 respondents from 27 countries, found that 86 percent of US participants use ASME Y14.5 and 56 percent of international participants also use ASME Y14.5. These numbers reflect the historical dominance of US manufacturing, defence, and aerospace programs in setting supply chain documentation standards globally. A German tier-two supplier working for a US aerospace prime must produce ASME-compliant drawings for that program regardless of what their domestic German customers require.

    The result is that many engineering teams outside the US maintain dual capability: ISO GPS for domestic and European customers, ASME Y14.5 for US and US-primed programs. This is manageable but requires explicit drawing management discipline, because the same part designed to two different standards requires two different drawings, and mixing elements from each into a single drawing creates the type of ambiguity that the shaft example at the beginning of this guide illustrates.

    World Map of Engineering Drawing Standard Dominance by Region

    The Title Block: Where the Standard Is Declared and Why It Must Be

    Every engineering drawing has a title block in the bottom-right corner. That title block is the drawing’s identity document, and it is also where the applicable drawing standard must be stated. Without an explicit standard reference in the title block or general notes, any GD&T on the drawing is ambiguous.

    What the Title Block Must State for Standard Compliance

    • Applicable GD&T standard: ‘Geometric tolerancing per ASME Y14.5-2018’ or ‘Geometric tolerancing per ISO 1101:2017’ — state the standard and the year of issue
    • General tolerance reference: ‘Unless otherwise specified, general tolerances to ISO 2768-mK’ or the equivalent ASME general tolerance note
    • Projection method: The first-angle or third-angle projection symbol — this should be graphic, not text, so it is recognisable internationally
    • Surface texture standard: If Ra values are used: ‘Surface texture per ISO 1302’ or ‘Surface texture per ASME B46.1’
    • Units: Millimetres or inches — never ambiguous, always stated
    • Material standard: The full material specification including the relevant standard (ASTM, DIN, EN, JIS) not just the alloy name

    ASME Y14.1 and ISO 7200: Title Block Format Standards

    ASME Y14.1 defines the drawing sheet sizes and title block requirements for ASME drawings. ISO 7200 defines the data field structure for title blocks on ISO drawings. DIN 6771 is the German supplementary title block standard.

    The field names in a DIN title block are often in German: ‘Werkstoff’ means Material, ‘Massstab’ means Scale, ‘Datum’ means Date, ‘Zeichen’ means Signature. An engineer unfamiliar with German who receives a DIN-format drawing from a German supplier will be able to read all the technical geometry but may misidentify which field contains the material specification versus the scale versus the date. Knowing the key field names in the languages of your main supplier countries is a practical working skill.

    Model-Based Definition: How Standards Apply in 3D Environments

    The engineering drawing is no longer always a 2D sheet. Model-Based Definition (MBD) embeds the tolerances, GD&T callouts, surface finish specifications, and material notes directly into the 3D CAD model as annotations, eliminating the 2D drawing entirely for some workflows.

    Both ASME and ISO have standards for MBD. ASME Y14.41 defines digital product definition data practices, including how 3D annotations are structured, what must be captured in the model, and how the model functions as a design authority without a 2D drawing. ISO 16792 covers the equivalent requirements under the ISO GPS framework.

    The standard selection question does not go away in MBD: it becomes more important, because the software that manages the 3D PMI (Product and Manufacturing Information) must be configured to apply the correct standard’s rules and defaults. CATIA, SolidWorks, NX, and Creo all support both ASME and ISO annotation modes, but the engineer must select the correct mode before applying tolerances to the model. A model annotated in ASME mode and interpreted by a supplier’s software in ISO mode will produce the same misinterpretation as a misread 2D drawing.

    Which Drawing Standard Should You Use? A Decision Framework

    This is the practical question that engineers and engineering managers actually need answered. The decision is not primarily technical. It is driven by the manufacturing context.

    Use ASME Y14.5-2018 when:

    • Your customer is a US aerospace or defence prime contractor
    • Your parts are inspected in the USA under ASME training and tooling
    • Your CAD system is configured with ASME defaults and your team is ASME-trained
    • The supply chain is primarily North American with US-standard inspection infrastructure

    Use ISO GPS (ISO 1101 and GPS family) when:

    • Your customer is European, particularly in Germany, France, Scandinavia, or other ISO-dominant markets
    • Your parts will be manufactured in Asia, where ISO standards are increasingly the baseline
    • The project involves international supply chains across multiple countries
    • Your team has ISO training and your CAD system is configured for ISO annotation

    Use DIN EN ISO when:

    • Your customer or program requires DIN references explicitly (common in German automotive and industrial machinery)
    • You are supplying into German automotive programs requiring VDA supplementary standards
    • The drawing must be formally compliant with German national adoption standards for procurement or regulatory reasons

    When your supply chain crosses standards:

    • State the governing standard explicitly in the title block. Do not leave it implicit.
    • If the drawing will be used by both ASME and ISO-trained engineers, produce two drawing sets or add a clear cross-reference note explaining which standard governs each section.
    • Train your suppliers in the standard you are issuing. Do not assume they know both.
    • Audit supplier inspection equipment and training against the standard you require. Gauges calibrated for ASME inspection may not be valid for ISO GPS inspection requirements.
    The one rule that prevents most cross-standard problems:  State the drawing standard in the title block on every drawing, every time. Not as a company logo or a footer note that gets overlooked. As a mandatory general note: ‘All geometric tolerances to ASME Y14.5-2018 unless otherwise stated.’ A two-second addition to the title block setup prevents the type of shaft rejection scenario described at the start of this guide.

    10 Engineering Drawing Standard Mistakes That Cause Real Manufacturing Problems

    These are the errors that show up most consistently in cross-border drawing reviews, supplier qualification audits, and failure investigations where the root cause traces back to a standards mismatch rather than a design error.

    MistakeConsequencePrevention
    Not stating the drawing standard in title blockManufacturer interprets GD&T under wrong standard. Form controls and datum behaviour differ.Always include a general note: ‘Unless otherwise specified, this drawing is to ASME Y14.5-2018’ or equivalent ISO/DIN reference.
    Reading a first-angle drawing as third-angleParts built with holes and features mirrored or on the wrong faceCheck the projection symbol in the title block before reading any view. Never assume.
    Mixing ASME and ISO symbols on one drawingAmbiguous or conflicting tolerance interpretationCommit to one standard per drawing. If global supply chain requires both, produce two drawing sets.
    Assuming ISO 2768 applies on an ASME drawingISO 2768 is not referenced in ASME. ASME uses its own general tolerance block.State the applicable general tolerance standard explicitly in the title block or general notes.
    Using concentricity from ISO on an ASME drawingConcentricity was deprecated in ASME Y14.5-2018. Coaxiality is now defined via position or profile.Use ASME-compliant controls for coaxiality: true position relative to datum axis, or profile of a surface.
    Assuming DIN 2768 and ISO 2768 are identicalThey are not. DIN 7168 and DIN 2768 have different tolerance classes and some different values.Check the exact DIN standard referenced on the drawing. Do not assume ISO equivalence without verification.
    Applying the independency principle to an ASME drawingForm errors are not separately controlled on ASME drawings by default. The envelope rule applies.For ASME drawings, if you need form independent of size, add the circle-E modifier explicitly to invoke independency.
    Ignoring the title block language on international drawingsDIN drawings from German suppliers will use German abbreviations (Werkstoffe, Massstab, Datum, Zeichen)Learn the key title block field names in the languages of your main supplier countries.
    Specifying Ra surface finish without stating the standardRa values are measured differently under ASME B46.1 and ISO 4287. The number is not directly comparable.State the applicable surface texture standard alongside the Ra value. Ra 1.6 per ISO 4287 is different from Ra 1.6 per ASME B46.1.
    Using old DIN standards superseded by ISO adoptionsOld DIN-only standards may reference values not in use at the supplierCheck whether the DIN standard cited has been replaced by a DIN EN ISO version. Many have since the 1990s harmonisation.

    Conclusion:

    The purpose of engineering drawing standards is to create a shared language between the person who designs a part and the person who makes or inspects it. ASME Y14.5, ISO GPS, and DIN standards all achieve this goal within their respective domains. The problems arise at the boundaries: when a drawing produced in one standard travels to a reader trained in another.

    The technical differences between ASME and ISO GPS are real and significant: the envelope vs independency principle changes what a size tolerance means. The deprecation of concentricity and symmetry in ASME Y14.5-2018 creates a live conflict with ISO GPS. The projection method difference produces mirrored or inverted parts if not checked. None of these differences are obscure. All of them are well-documented in the respective standards. The problem is that they only become visible at the moment the wrong assumption is applied to the wrong drawing.

    The prevention is straightforward: state the applicable standard in the title block. Check the projection symbol before reading views on an unfamiliar drawing. Never assume that the same symbol means the same thing under a different standard without verifying. And when working across standards in a global supply chain, treat the standards gap as a project risk to be managed explicitly, not a detail to be resolved by whoever is holding the drawing when the question arises.

    State the standard. Check the projection. Verify the defaults. Every time.

    Frequently Asked Questions

    What is the difference between ASME and ISO engineering drawing standards?

    ASME standards, primarily ASME Y14.5, govern engineering drawings in the USA and North America and use third-angle projection. ISO standards, the GPS (Geometrical Product Specifications) system centred on ISO 1101, are the international standard used in Europe, Asia, and globally, and use first-angle projection. The most significant technical difference is tolerancing philosophy: ASME uses the envelope principle where size controls form by default, while ISO GPS uses the independency principle where form must be explicitly controlled with separate symbols. Some GD&T symbols also differ: concentricity and symmetry were deprecated in ASME Y14.5-2018 but remain in use under ISO.

    What does DIN stand for in engineering drawings?

    DIN stands for Deutsches Institut fur Normung, which is the German Institute for Standardization. DIN standards for engineering drawings have been largely harmonised with ISO since the 1990s, and most current DIN drawing standards are cited as DIN EN ISO, meaning the German national adoption of an international ISO standard. DIN standards remain particularly influential in German automotive supply chains (VDA requirements), precision machinery, and industrial equipment sectors where German-originated specifications are common.

    What is third-angle vs first-angle projection on an engineering drawing?

    Third-angle projection is used on ASME and ANSI drawings, primarily in the USA. In third-angle, each view is placed on the same side as the direction you are looking from: the top view sits above the front view, and the right side view sits to the right. First-angle projection is used on ISO and DIN drawings, primarily in Europe and Asia. In first-angle, each view is placed on the opposite side: the top view sits below the front view, and the right side view sits to the left. A small symbol in the drawing title block identifies which projection is used. Misreading one as the other produces parts with features on the wrong faces.

    What is the envelope principle in ASME Y14.5?

    The envelope principle, also called the Taylor principle, is ASME Y14.5’s default rule for size tolerances. It states that the size tolerance limits of a feature also control the maximum variation in form. A shaft with a diameter tolerance of 25mm plus or minus 0.1mm cannot exceed a perfect cylinder of 25.1mm diameter at any cross-section. This means size tolerances implicitly control straightness and circularity without requiring additional GD&T symbols. ISO GPS uses the opposite default: the independency principle, where size and form errors are controlled independently. ISO requires explicit GD&T callouts to control form even on simple sized features.

    Which drawing standard is used in aerospace?

    US aerospace programs follow ASME Y14.5-2018 as the primary GD&T standard, supplemented by ASME Y14.100 for drawing practices and ASME Y14.41 for Model-Based Definition. European aerospace programs follow ISO GPS standards aligned with EN 9100 quality requirements. Multinational programs, such as those where US OEMs work with European suppliers, sometimes require drawings to comply with both, which is one of the most challenging aspects of global aerospace supply chain management. The drawing must explicitly state which standard applies to avoid ambiguity.

    Can ASME and ISO GD&T symbols be used on the same drawing?

    Mixing ASME and ISO GD&T symbols on the same drawing without explicit notation creates serious risk of misinterpretation because the same symbol can mean different things under different standards, and default assumptions differ significantly. Concentricity is a direct example: the symbol exists in ISO but has been deprecated in ASME Y14.5-2018. If a drawing must be used in both ASME and ISO manufacturing contexts, the safest approach is to produce two separate drawing sets, one referencing each standard, or to add a prominent general note specifying which standard governs all GD&T callouts.


    ‘asme.org/codes-standards/find-codes-standards/y14-5-dimensioning-tolerancing‘